The salt spray test is an accelerated corrosion test that reproduces an aggressive, controlled saline atmosphere inside a sealed chamber, forcing in hours or days the deterioration a metal or coating would take months or years to reveal outdoors. It does not copy real weather point by point: it holds constant, severe conditions so you can compare finishes, expose weak points in a protective layer and classify the degree of degradation against repeatable criteria.
Running it with any confidence takes a calibrated chamber, stable parameters and pass/fail criteria fixed in advance, which is exactly what an industrial engineering laboratory equipped for corrosion work provides. When the goal is to choose between finishes or validate a purchasing specification, the corrosion assessment and protection service supplies the technical framework that turns raw exposure hours into a defensible decision about the material.
What the salt spray test simulates
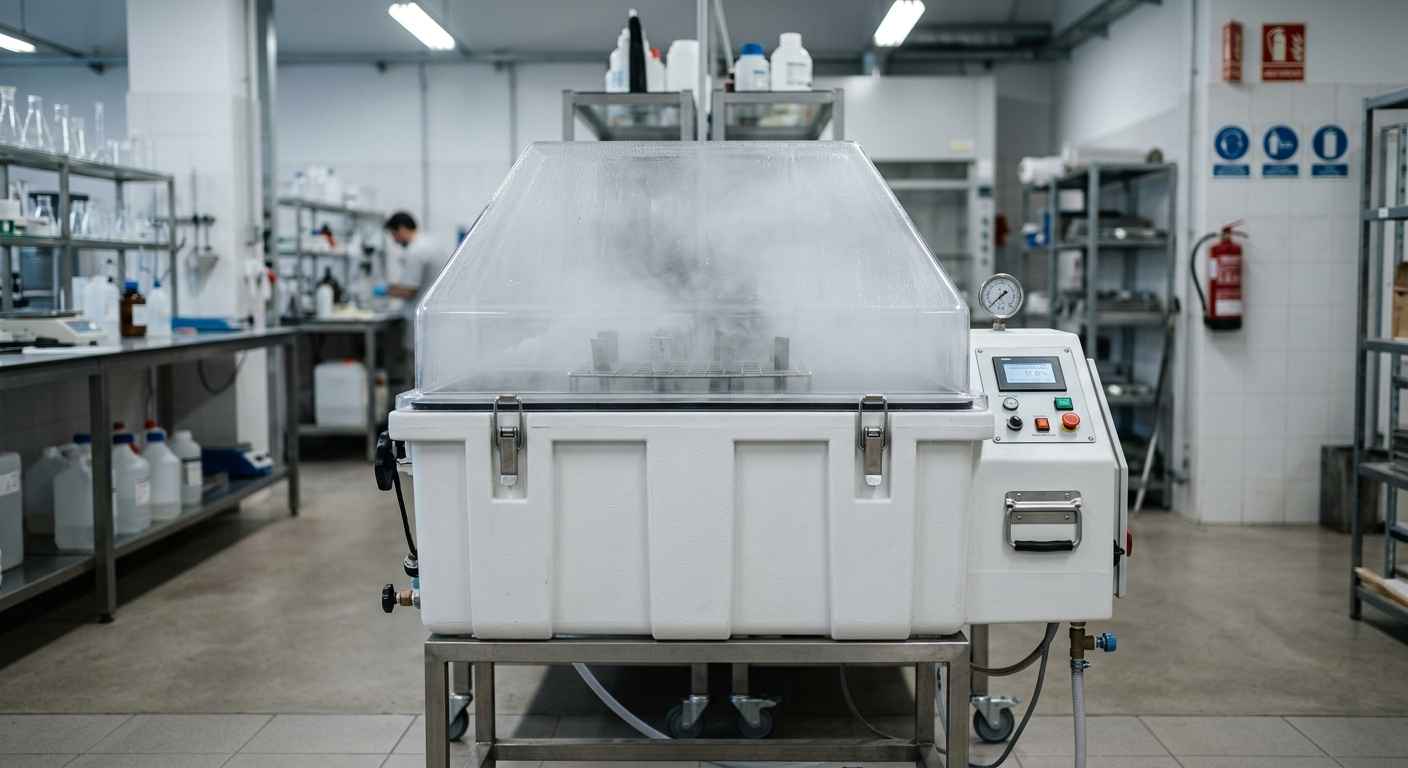
The salt spray test simulates the combined action of permanent moisture and chlorides on a metallic or coated surface, that is, the electrochemical corrosion mechanism that appears in marine environments, on roads treated with de-icing salts and in industrial atmospheres loaded with saline aerosols. Inside the chamber, a sodium chloride solution is atomised continuously into a fine mist that settles on the specimens and keeps the surface wet and salty for the full duration of the run.
A standardised aggressor, not a real climate
What it reproduces is therefore not a specific climate or a real location, but a standardised aggressor. Chloride ions break down passive films with ease and work their way into pores, microcracks and coating edges, accelerating rust formation wherever the protection is thin. That constant aggressiveness is at once the method’s strength and its limit: it guarantees that two runs are comparable, but it gives up any attempt to imitate the wetting, drying and sunlight cycles that govern corrosion in the open air. In real weather, the drying periods let many metals build up a relatively stable layer of corrosion products that slows the later attack; by keeping the surface permanently wet, the salt spray chamber prevents that protective layer from maturing and sustains the electrochemical mechanism at a pace nature rarely delivers without interruption. That is why the test accelerates so much and, at the same time, why its hours do not translate directly into service time. A finish either holds the aggressor back or it does not, and the chamber shows you where the first breach happens.
The salt spray test does not tell you how many years a part will last; it quickly reveals where its corrosion protection fails and lets you rank finishes against one another under identical conditions.
A comparison and quality-control tool
That constant aggressiveness makes the method a tool for comparison and quality control rather than a direct prediction of service life. It ranks finishes against each other, flags a coating lot that falls outside specification and confirms that a supplier meets what was agreed, always under the same aggressor and the same conditions. This test belongs to the wider family of corrosion and surface characterisation methods applied during testing of metallic materials and alloys, where resistance to a saline environment is just one of the parameters that define in-service behaviour. Treat it as one link in a validation plan, not as a standalone verdict on durability.
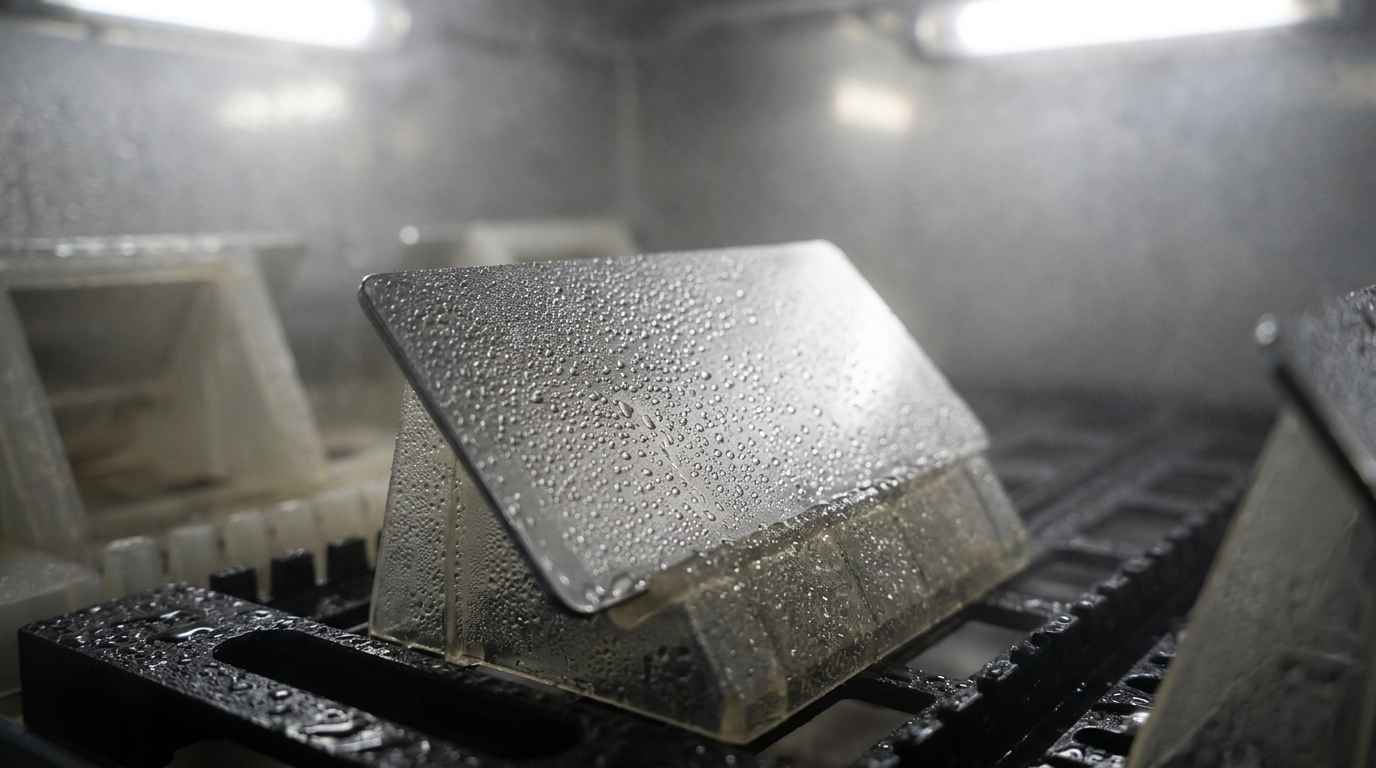
How the chamber works and the test variants
A salt spray chamber is a sealed enclosure that controls temperature, salt concentration, solution pH and mist deposition rate so that every specimen receives the same exposure. ISO 9227 sets out how to run the test: the neutral variant uses a 5% sodium chloride solution atomised at 35 °C, with a pH between 6.5 and 7.2 and a deposition rate of 1 to 2 ml per hour collected over an 80 cm² horizontal surface. These figures are not arbitrary; they are what makes a result obtained in one laboratory comparable with a result obtained in another.
Parameters the chamber controls
Specimen placement is regulated too. Panels are tilted 15 to 25 degrees from the vertical so the mist deposits evenly and droplets neither pool nor run off unequally. Any drift in the tilt angle, in the atomising air pressure or in the purity of the water changes the real aggressiveness of the environment and undermines the comparability of the data. Stability across the whole exposure, including overnight hours and the brief openings for inspection, is what separates a valid test from one that merely generates rust with no diagnostic value. A drop in temperature slows the reaction; an excess of concentration drives it in a way that no longer represents the intended severity. The pH of the solution deserves particular vigilance, because it tends to drift during exposure and a small shift is enough to change the rate of attack, so it is checked periodically and corrected if it strays from the band the standard sets. The mist is also generated with humidified air through a saturation tower, whose job is to keep the compressed air from drying out the atomised solution or altering its concentration as it enters the chamber. And the deposition rate is not assumed: it is measured by collecting the settled mist in standardised collectors over a known interval, so the amount of salt reaching the specimen is documented rather than left to the operator’s judgement.
The NSS, AASS and CASS variants
Three main variants exist, chosen by how aggressive the environment needs to be and what material is under evaluation. Neutral salt spray (NSS) uses plain sodium chloride and is the general reference for steels, galvanised parts and organic coatings. Acetic acid salt spray (AASS) acidifies the solution to a pH near 3.2 and targets decorative copper-nickel-chromium coatings and anodised surfaces. Copper-accelerated acetic acid salt spray (CASS) adds copper chloride and raises the temperature to 50 °C, intensifying the attack and shortening test times for demanding finishes. Each variant drives a different deterioration mechanism, so choosing the wrong one voids any comparison with the specification. Selecting the right one usually leans on analysis of galvanized, anodized and coated materials, which helps explain why one finish resists and another gives way under the same mist.
Have a similar case on your desk?
If you want to discuss it with our technical team, the first conversation is with no obligation.
How exposure hours are interpreted
Exposure hours state how long a specimen has withstood the saline environment before reaching a predefined failure criterion, not a number of real-life years. Reading them well starts by accepting that distinction and by fixing in advance what is being measured.
What a figure of hours really measures
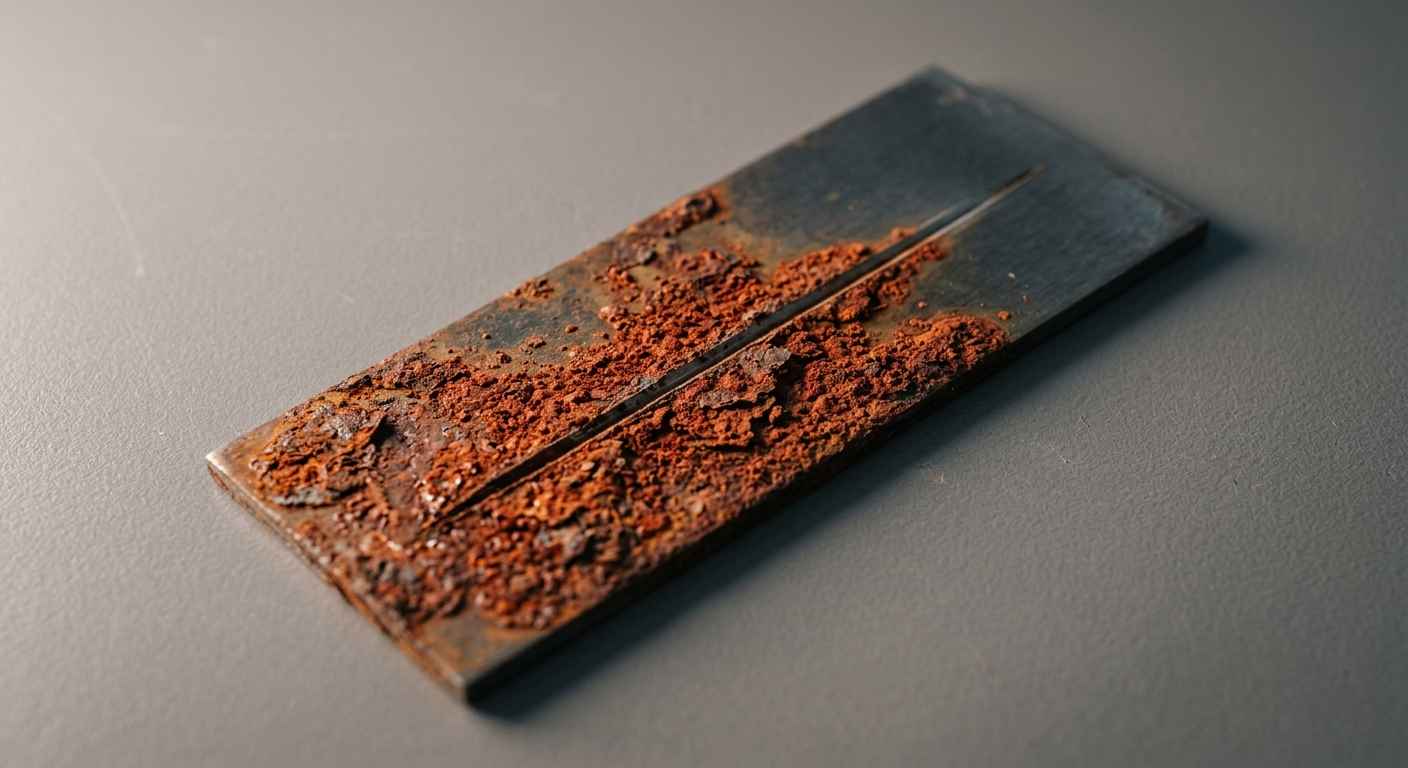
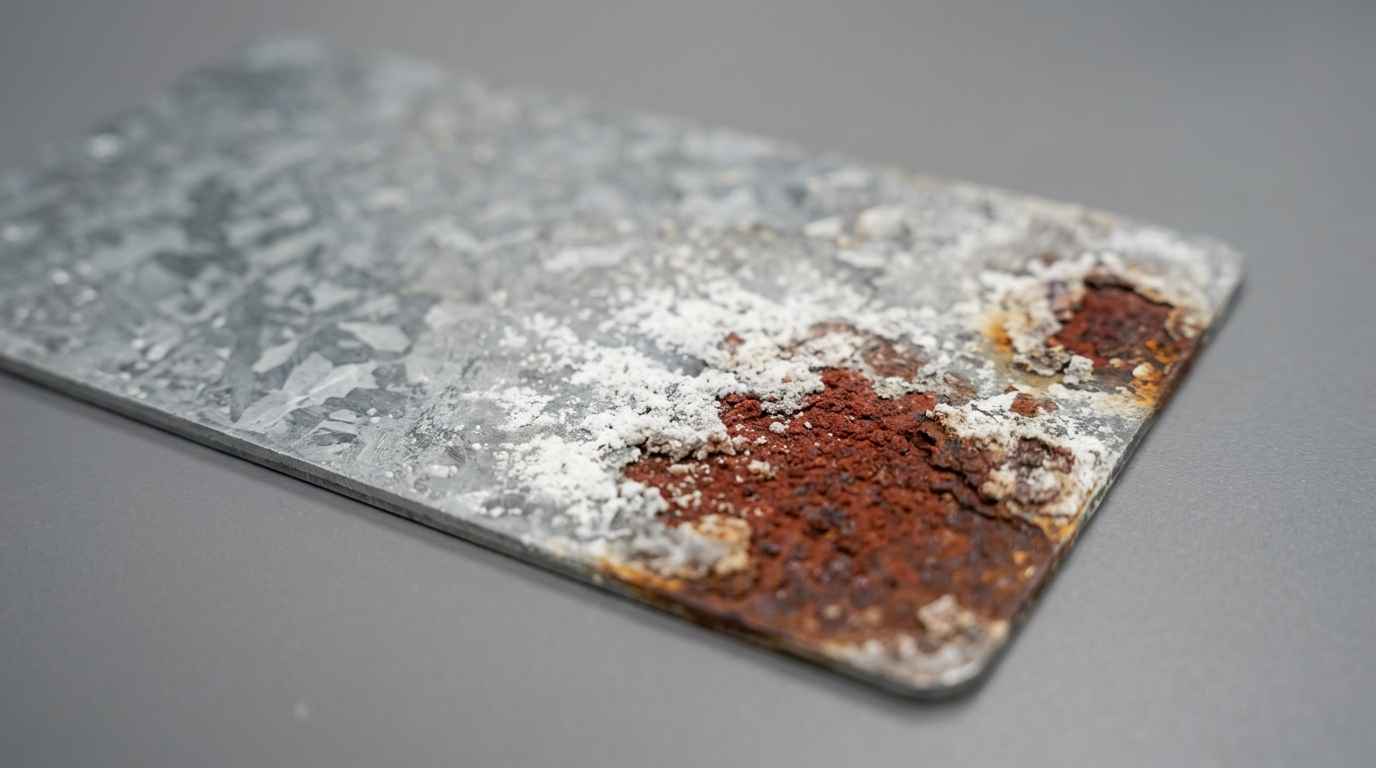
Saying a coating “survives 500 hours” only means something once you specify the failure you were looking for: the first point of red rust, a percentage of corroded area, blistering, or the spread of corrosion from a deliberate scribe cut in the coating (scribe or scratch-creep assessment). The correlation between chamber hours and years of service is imperfect and depends on the material, the finish and the real environment of use. No universal conversion factor is reliable: a ratio that holds for galvanised steel in a marine atmosphere does not transfer to an interior paint coating. Hours are therefore used mainly to rank finishes against each other and to verify compliance with a specification, never as an absolute prediction of durability. The type of failure chosen also shapes the figure: on a galvanised part it is common to distinguish between the onset of white rust (attack on the zinc coating) and red rust (once the base steel is exposed), and fixing which of the two counts as failure changes the declared hour count entirely. In the scribe test, what is measured is not only when corrosion appears but how far it creeps sideways beneath the coating from the cut, a parameter that reveals the adhesion and the layer’s ability to contain deterioration once it starts. Documenting precisely which criterion was applied is what stops two laboratories from reporting different figures for the same part.
The standardised scales of ISO 4628
Assessing the degree of degradation relies on ISO 4628, which provides standardised scales to quantify defects such as blistering, rusting, cracking and flaking by assigning a quantity and a size to each defect type. Applying these scales turns a subjective visual inspection into a repeatable rating that different assessors can reproduce, which is precisely what lets a “pass” or a “fail” mean the same thing in the laboratory and at the customer. Each defect is graded on a discrete scale that captures both how much of the surface is affected and how large the individual defects are, so a coating with a few large blisters and one with widespread fine blistering are not lumped into the same verdict. Photographic reference charts anchor each grade, which is what keeps two assessors, or the same assessor months apart, from drifting toward different numbers on visually similar panels.
| Test variant | Fluid / conditions | Temperature | Typical use |
|---|---|---|---|
| NSS (neutral salt spray) | 5% NaCl, pH 6.5–7.2 | 35 °C | Steels, galvanised parts, organic coatings |
| AASS (acetic acid salt spray) | 5% NaCl + acetic acid, pH ~3.2 | 35 °C | Decorative Cu-Ni-Cr coatings, anodised surfaces |
| CASS (copper-accelerated acetic acid) | 5% NaCl + CuCl₂ + acetic acid, pH ~3.2 | 50 °C | High-demand finishes, most aggressive and fastest run |
Once variant, duration and failure criterion are fixed, the outcome reads as a comparative rating. An accelerated corrosion test used to optimise laser marking shows how that reading can steer a process rather than just close it: the mist does not only pass or reject a part, it can guide the tuning of a manufacturing parameter when combined with analysis of the affected surface.
Reading the hours correctly means fixing the failure criterion and the ISO 4628 rating scale in advance; without that reference, the same exposure time can be judged a success or a rejection depending on who looks at it.
What the test does not prove and interpretation mistakes
The salt spray test does not prove the real durability of a part in its service environment, because it subjects the material to a constant, uniform atmosphere that ignores the wet-dry cycling, solar radiation, temperature swings and atmospheric pollutants that speed up or slow down corrosion in practice. A finish that clears 1,000 hours of mist can behave worse in the field than one with fewer hours if the real environment combines thermal cycling with ultraviolet exposure. The mist measures resistance to a single aggressor, chloride under wet and constant conditions, while in-service deterioration is usually the result of several mechanisms that overlap and reinforce one another.
Common interpretation mistakes
The most common mistake is treating hours as a direct equivalent to years of use. The second is comparing results from different variants (NSS against CASS) as though they shared one scale. The third is ignoring the effect of part geometry: edges, welds, bolted joints and water-trapping pockets corrode before a flat surface does, and a smooth panel never captures that behaviour. Galvanic corrosion is underestimated just as often, arising wherever two dissimilar metals meet in the presence of the saline electrolyte. A fourth, subtler error is neglecting specimen preparation: unprotected edges, handling marks or grease residues introduce initiation points that do not reflect the real finish and contaminate the result. A result misread through any of these traps can approve a finish that will fail in service, or reject one that is perfectly sound, so the correct reading always starts from the question you meant to answer.
When to combine the test with other methods
Understanding the failure mode is what closes the gap. Just as fractography distinguishes brittle and ductile fracture to explain why a component gives way, corrosion analysis has to separate a localised coating defect from an adhesion problem or a generalised attack. The hour count alone tells none of that story. The test performs best inside a plan that adds ultraviolet ageing, climatic cycling and analysis of the part’s real behaviour against external agents, so the saline result is read in context rather than in isolation. When the aim is to improve a finish and not merely check it, the work reaches into the full protection system, as in an evaluation of steel coatings to improve corrosion resistance, where the mist result is crossed with characterisation of the protective layer to explain the failure mechanism, not just record it.
From a number of hours to an evidence-based material decision
The salt spray test gives you a fast, repeatable and comparable measure of how a surface resists chloride attack, yet its real value emerges only when you fix the right variant, the failure criterion and the rating scale in advance, and when you read the hours as a comparison rather than a forecast of years. Set up that way, it lets you choose between finishes, validate a purchasing specification and catch weak points in a protective layer before the part reaches the market. Where it fits within a broader validation strategy is best decided alongside accelerated ageing tests that add the environmental loads the chamber leaves out.
The distance between a salt spray figure and a sound decision lies in the interpretation: tying the hours to the degradation mechanism, checking them against the real environment of use, and combining them with other methods when the material demands it. If you have panels, coated parts or a finish you need to compare or validate against corrosion, send your samples together with the specification and the intended service environment, and you will receive a test run to standard with a technical reading of what the hours actually mean for your case.
Frequently asked questions about the salt spray test
What does the salt spray test simulate?
The salt spray test simulates an aggressive, constant saline environment that accelerates the corrosion of metals and coatings, reproducing the effect of the chlorides present in marine atmospheres, de-icing salts or industrial settings. It does not copy a real climate; it creates a standardised aggressor so you can compare finishes and expose where the protection fails in a repeatable way.
How many salt spray hours equal years of use?
No reliable universal equivalence exists between salt spray hours and years of use, because the correlation depends on the material, the finish and the real service environment. The hours serve to rank finishes against each other and to verify compliance with a specification, not to predict exact service life. Estimating real durability requires combining the test with climatic cycling and ultraviolet exposure.
What is the difference between NSS, AASS and CASS?
NSS, AASS and CASS are three variants of differing aggressiveness. NSS uses neutral sodium chloride and is the reference for steels and galvanised parts; AASS acidifies the solution with acetic acid for decorative coatings and anodised surfaces; CASS adds copper chloride and raises the temperature to 50 °C for high-demand finishes. Each drives a different deterioration mechanism, so their results are not interchangeable.
Does the salt spray test measure real service life?
The salt spray test does not measure a part’s real service life, because it applies a uniform, continuous environment that omits the wet-dry cycling, solar radiation and thermal swings of the real setting. It is a comparison and quality-control tool; to estimate durability, integrate it into a plan with accelerated ageing and analysis of behaviour against external agents.
Which standards govern the salt spray test?
Execution of the salt spray test is governed mainly by ISO 9227, which defines salt concentration, temperature, pH and deposition rate, while the assessment of the degree of degradation relies on ISO 4628. Internationally, the ASTM B117 specification is also used as an equivalent reference for the neutral salt spray test.